If you’ve ever stood in a manufacturing plant, wastewater treatment facility, or building with complex piping systems, chances are you’ve walked past a lift check valve without noticing it. As a lift check valve supplier, I talk to contractors, maintenance technicians, and plant operators every week who assume the valve’s body or the pipe it’s installed in does all the heavy lifting—until a line breaks, backflow ruins a batch of product, or a pump burns out because reverse flow snuck through an unprotected line. The disc is the quiet, unassuming hero inside every lift check valve, and understanding its function isn’t just a technical detail—it’s the difference between avoiding costly downtime and navigating a preventable emergency. Lift Check Valve
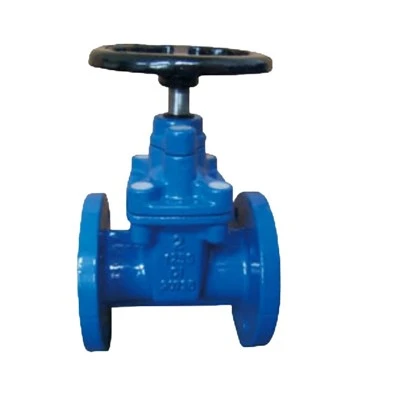
Let’s start with the basics to set the stage. A lift check valve is a type of non-return valve, designed specifically for systems where flow runs in one direction during normal operation but could reverse if pressure shifts. Unlike swing check valves that use a hinge and flapper, lift check valves have a disc that moves straight up and down along a guided stem, sitting flush against a seat when closed. That vertical motion is non-negotiable for its core function. When fluid flows forward, it pushes the disc up off the seat, opening the valve to let product pass. As soon as forward flow slows or stops—like when a pump shuts down, or downstream pressure spikes—the disc falls back down to seal the seat tight, stopping reverse flow in its tracks. Simple, right? But the nuance of that disc’s design is where it delivers real value to any piping system.
First and foremost, the disc’s primary function is backflow prevention. That’s the whole reason lift check valves exist, but it’s worth breaking down why the disc is the only component that can execute that task reliably. I’ve seen too many systems where a poorly maintained or mismatched disc leads to backflow. For example, at a food processing plant I visited last year, a contractor installed a lift check valve with a disc made from the wrong rubber compound. The sanitizing solution used during overnight maintenance ate through the disc, leaving a small gap that let residual product flow backward into the water supply line. By the time maintenance crews caught the problem, 500 gallons of finished goods were contaminated, and the plant was down for 12 days. That’s the cost of overlooking the disc: it’s not just a piece of metal or rubber—it’s the final barrier between your product, your equipment, and safety hazards.
Beyond backflow prevention, the disc also acts as a flow regulator, even if that’s a secondary function. Because it moves only vertically along a guided stem, it lifts in direct proportion to the pressure of forward flow. That means at low flow rates, the disc only lifts partially, creating a smaller opening that keeps flow velocity consistent. At high flow rates, it lifts fully to maximize the pipe’s opening, reducing turbulence and pressure drop. Turbulence is a big deal in high-pressure systems, like those used in oil and gas pipeline stations or municipal water distribution. Too much turbulence can erode pipe walls, cause vibrations that loosen fittings, or even damage the pump itself, which has to work harder to overcome those pressure gaps. I had a customer in the mining industry tell me they replaced their old check valves a few years back because the swing-type disc in their system created so much vibration that it cracked a 6-inch pipe every six months. Since switching to lift check valves with precision-machined discs, they haven’t had a single crack in two years. That’s the disc’s function at work: smoothing flow to extend the life of the entire system.
Another critical function of the disc is wear resistance, which is tied directly to how it interacts with the seat and the fluid passing through it. The disc sits on the valve’s seat, a matching ring made of the same or compatible material to create a tight seal when closed. Every time the disc lifts or falls, it has to make contact with the seat without causing excess wear, and every time it’s in the open position, it has to resist abrasion from suspended solids—common in wastewater, mining slurries, or even water with mineral deposits. As a lift check valve supplier, we design our discs with material-specific coatings and shapes tailored to the application: for abrasive slurries, we use stainless steel discs with a hard chrome plating that resists scratching; for corrosive chemical lines, we offer PTFE or EPDM rubber discs that won’t degrade in acidic or alkaline solutions. A bad disc that wears out quickly won’t seal properly, leading to the same backflow problems I mentioned earlier, but it also means premature valve replacement, which adds up fast for large facilities with dozens or hundreds of check valves.
Wait, some people might ask—why not just use a gate valve or a ball valve to stop reverse flow? The answer is timing. Lift check valves, thanks to their disc design, close almost instantly when flow reverses. Gate and ball valves require manual operation or an external actuator, which means there’s a delay between when flow slows and when the valve is closed. In many systems, that split second of reverse flow is enough to cause major damage. For example, a centrifugal pump’s impeller is designed to push fluid forward; if reverse flow hits it before the pump comes to a complete stop, the impeller can reverse direction, leading to metal fatigue and eventual failure. I’ve seen pump replacements cost 10 times more than a lift check valve, all because the wrong valve couldn’t respond fast enough. That’s the disc’s real superpower: it’s a passive component, powered entirely by the flow of fluid, so it reacts to pressure changes in milliseconds, no electricity or manual input needed. That reliability is why lift check valves are the go-to for critical systems like fire sprinkler lines, pharmaceutical processing, and HVAC systems that serve large commercial buildings.
Of course, the disc isn’t perfect—and its function depends entirely on how it’s sized, installed, and maintained. A common mistake I see is oversizing the disc to match a larger pipe, which means the disc doesn’t lift all the way, creating partial restriction and more turbulence. Or undersizing the disc, which means it closes too quickly, causing water hammer—a sharp pressure spike that can rupture pipes, burst fittings, or knock valves loose. I had a customer in a high-rise apartment building call me a few years back, panicking because their water pipes were banging every time the elevator pressure pump shut off. They had installed lift check valves with discs that were 2 inches too small, so the disc would slam shut the second flow stopped, causing a water hammer event loud enough to disturb residents on the 10th floor. Once we sized the discs correctly and adjusted the spring tension on the valve (another detail tied to disc function), the noise stopped completely. That’s a perfect example of how the disc’s function is only as good as the rest of the valve’s design.
Another thing to note is the role of the disc’s seal integrity in potable water systems. For facilities that supply drinking water, like municipal water treatment plants or food and beverage manufacturers, the disc has to create a 100% leak-proof seal to prevent backflow of non-potable water into the clean supply. A worn or damaged disc can lead to cross-contamination, which is not only a health risk but also a legal one. In the U.S., the EPA has strict standards for backflow prevention in potable water lines, and lift check valves are often a key component of those systems. Our company’s discs for potable water lines are certified to NSF/ANSI 61 standards, which means they’re non-toxic and won’t leach chemicals into the water supply. That’s a non-negotiable part of the disc’s function in critical applications: it’s not just about flow control, it’s about public health and safety.
Let’s talk about maintenance, too—because even the best disc will wear out over time, and understanding its function helps with proactive upkeep. Most maintenance technicians only check the valve body and the pipe, but the disc should be inspected annually (or more often in high-abrasion or high-corrosion systems). What do you look for? Scratches, gouges, or warping on the disc’s sealing surface; wear on the stem that guides the disc; and proper alignment between the disc and the seat. If the disc is scratched, it won’t seal tight, leading to backflow. If it’s warped, it might not close all the way, leaving a gap. I’ve had customers tell me they wait until the valve starts leaking before checking the disc, which is like waiting for a flat tire to check the air pressure—by then, the damage is already done.
As a lift check valve supplier, I talk to a lot of people who are new to specifying or maintaining these valves, and the biggest misconception is that all discs are the same. They’re not. A disc designed for a wastewater line won’t work in a pharmaceutical line, and a disc made for low-pressure water won’t hold up in a high-pressure gas line. That’s why taking the time to understand the disc’s function for your specific application is so important. It’s not a one-size-fits-all component. When I work with a customer, I always ask about their system’s pressure, flow rate, fluid type, and environment before recommending a disc and valve combination. That personalization is what makes the difference between a valve that works for a few months and one that lasts for years.
Looking ahead, as piping systems get more complex—with smart monitoring, variable flow rates, and stricter environmental standards—the disc’s function will only become more important. New designs are already emerging, like self-lubricating discs that reduce wear in high-cycle systems, and micro-machined discs that create even more consistent flow in low-pressure lines. But the core function remains the same: to prevent backflow, regulate flow, and protect the entire system from damage.

At the end of the day, the disc in a lift check valve is easy to overlook. It’s hidden inside the valve body, out of sight and out of mind—until something goes wrong. That’s why I always tell my customers: don’t underestimate the small parts. The disc is the barrier between your product, your equipment, and costly downtime. If you’re specifying new lift check valves, replacing old ones, or dealing with backflow issues in your system, don’t guess at the right disc size or material. Reach out to our team to discuss your specific needs, and we’ll help you find the right components to keep your system running smoothly. Whether you’re in manufacturing, municipal water management, or industrial processing, getting the disc right is the first step to a reliable piping system.
Globe Valve By Structure Type References:
- Bleier, F. P. (1998). Pump Handbook. McGraw-Hill Education.
- American Water Works Association (AWWA). (2019). Backflow Prevention and Cross-Connection Control Manual. AWWA.
- Karassik, I. J., Messina, J. P., Cooper, P., & Heald, C. C. (2008). Pump Handbook (4th ed.). McGraw-Hill.
- NSF International. (2022). NSF/ANSI Standard 61: Drinking Water System Components – Health Effects. NSF International.
- Mining Equipment and Technology Association (META). (2021). Mining Piping System Reliability Guidelines. META.
Yantai Valtone Valve Co., Ltd.
As one of the most professional lift check valve manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy bulk durable lift check valve for sale here from our factory. We also accept customized orders.
Address: No. 13, Wuhan street, Bajiao industry park, Yantai ETDZ, Shandong, China.
E-mail: liujun@valtone-valve.com
WebSite: https://www.valtonevalve.com/
