As a centrifugal barrel finishing machine supplier, I get a lot of questions from metal finishing shop owners, production managers, and lead operators. Most of the queries start the same way: “My finishing results are great, but my team is dealing with headaches by the end of the day, and I’m worried about dust buildup in the plant.” It’s a valid concern—centrifugal barrel finishing (CBF) machines are workhorses for deburring, polishing, and finishing small, high-volume metal parts, but they also generate fine metal dust, chemical fumes from finishing compounds, and even airborne debris from tumbled media. Proper ventilation isn’t just a workplace comfort issue; it’s critical for worker safety, equipment longevity, and consistent finishing quality. Over the past 12 years I’ve worked with CBF users across automotive, aerospace, and medical parts manufacturing, I’ve learned that ventilation for these machines isn’t a one-size-fits-all fix. It needs to be tailored to your machine’s size, the parts you process, and the finishing compounds you use. Let’s break down how to get it right. Centrifugal Barrel Finishing Machine
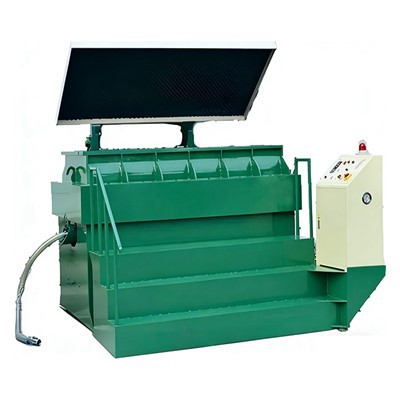
First, it’s important to understand exactly what a CBF machine releases into the air during operation. Unlike rotary tumblers that spin slowly, centrifugal barrel machines rotate their barrels around a central axis at high speeds—sometimes 60 to 200 RPM—while the barrels themselves spin in the opposite direction. That high-speed motion flings small particles: metal shavings from deburring ceramic or plastic media worn down during polishing, and volatile organic compounds (VOCs) from water-based or chemical finishing compounds that break down as the barrels churn. For example, a shop processing 10,000 small aluminum valve covers per batch will generate far more fine aluminum dust than a shop polishing stainless steel screws in smaller batches. I remember a customer in Detroit who ran three medium-sized CBF machines side-by-side finishing steel engine parts. They initially had their general warehouse ventilation running, but after a month, their air quality tests showed 2.2 milligrams of respirable crystalline silica per cubic meter—well over the OSHA limit of 0.05 mg/m³ for an 8-hour shift. Their operators were complaining about dry throats and eye irritation, and one of their CBF machine’s motor housings had a dust buildup that caused it to overheat and fail prematurely. That’s when we walked them through specific ventilation steps, and within two weeks, their air quality was compliant, and they replaced the failed motor without extra downtime.
The first step to ensuring proper ventilation for your CBF machine is to match your ventilation system to your machine’s design and throughput. Not all CBF machines are the same. If you have a benchtop CBF machine for small, low-volume jobs, you don’t need a 5,000 CFM (cubic feet per minute) exhaust hood. For large, industrial CBF machines with 50-gallon or larger barrels running 24/7, a general wall vent isn’t enough. Here’s what I recommend based on our experience as a supplier: For enclosed CBF machines—those with a sealed cabinet around the rotating barrels—install a localized exhaust vent that connects directly to the machine’s built-in dust outlet, if it has one. Most industrial CBF machines we sell come with a pre-plumbed port for this exact purpose, but many shops don’t connect it. This localized vent pulls air and contaminants directly from the source, before they spread into the work area. We once visited a medical parts shop in Minneapolis that used an older CBF machine without a built-in port. They were processing titanium hip stems, which generate extremely fine, easily inhaled metal dust. We worked with their maintenance team to mount a 1,200 CFM flexible exhaust hood 6 to 12 inches above the machine’s loading door (the point where they open it to add parts and media). That setup cut their airborne titanium dust levels by 78% in their initial air quality test.
For open-top or partially enclosed CBF machines—common in shops that process very large parts or mixed batches of materials—localized ventilation needs to be paired with a properly sized general room ventilation system. The rule of thumb we use here is to calculate the total air change rate for your finishing room. For shops with high-contamination finishes (processing ferrous metals, titanium, or using solvent-based compounds), the room should have 6 to 8 full air changes per hour. For shops working with non-ferrous metals and water-based finishing compounds, 4 to 5 air changes per hour is sufficient. But a common mistake we see is shops setting their ventilation to pull too much air, which can actually disrupt the CBF machine’s barrel motion. Centrifugal barrel machines rely on a consistent, gentle flow of media and parts to get uniform finishing. If your ventilation pulls too much air through the room, it can create a draft that tilts the barrel, leading to uneven tumbling—so you’ll have some parts over-finished, some under-finished, and wasted finishing compound. We helped a customer in Chicago who adjusted their ventilation to pull 10 air changes per hour, and their finishing quality dropped by 15% in a week. When they dialed it back to 6, their results went back to normal, and their air quality stayed compliant.
Next, choosing the right type of air filtration for your ventilation system is non-negotiable. A lot of shops install an exhaust fan and call it a day, but without proper filtration, you’re just moving contaminated air from one part of the plant to another, or even releasing it outside where it can harm local air quality and even get you cited by environmental regulators. For CBF machines, there are two main levels of filtration you need: pre-filtration and final HEPA or activated carbon filtration. Pre-filters are larger, more durable filters that catch the biggest particles—media fragments, large metal shavings, and clumps of finishing compound. They should be changed every 2 to 4 weeks, depending on your throughput. Final filters are designed for fine particles and fumes. For metal dust, a HEPA filter is necessary to catch 99.97% of particles 0.3 microns and smaller—this includes respirable particles that cause long-term health issues. For VOCs from chemical compounds, activated carbon filters will absorb these fumes before they’re released. We’ve tested different filter brands with our customers, and we always recommend choosing filters rated for continuous use in industrial settings, not residential ones. One customer in Dallas used residential filters for their CBF ventilation and noticed that after a month, the filters were clogged with fine aluminum dust, which reduced their fan’s airflow by 40% and caused their machine’s motor to work harder, leading to higher energy bills. Swapping to industrial-grade filters fixed that issue, and their energy use went down by 12% right away.
Another often-overlooked factor is air make-up. When you install an exhaust system to pull contaminated air out of your finishing room, you need to replace that air with clean, conditioned air—otherwise, you’ll create negative pressure in the room, which can pull dust and fumes from adjacent areas (like your assembly line or warehouse) into the finishing area, or even cause doors or machine access panels to slam shut unexpectedly. Air make-up should be delivered at a rate that’s 80 to 90% of your exhaust rate, to keep the room at a slightly negative pressure (0.02 to 0.05 inches of water column) relative to the rest of the plant. This way, no contaminated air leaks out, and you don’t have drafts disrupting your CBF machine. A customer in Phoenix learned this the hard way last year. They had a large industrial CBF machine running 16 hours a day, and their exhaust system pulled 5,000 CFM of air out of the finishing room, but they only added 1,000 CFM of make-up air. Their room was so negative that dust was seeping through the gaps in the machine’s cabinet, and their operators had trouble opening the machine’s loading door—they had to use a crowbar to pry it open on some days. Adding 4,000 CFM of conditioned make-up air fixed that problem, and they also noticed that their machine’s finishing consistency improved, because the barrel motion was no longer being disrupted by the negative pressure pulling on it.
Regular maintenance of your ventilation system is just as important as installing it correctly. Even the best ventilation setup won’t work if the filters are clogged, the fan is broken, or ductwork is blocked. We include a free 10-point ventilation maintenance checklist with every CBF machine we sell, and we recommend that customers follow it every month. The checklist includes: checking pre-filters for clogs and replacing them if needed, testing fan airflow with a basic anemometer to ensure it’s running at the rated CFM, inspecting ductwork for dust buildup or blockages (we’ve seen dust clumps the size of basketballs in ductwork that wasn’t cleaned for a year), and testing air quality monthly (using a small handheld monitor for respirable dust and fumes). We also recommend scheduling a professional ventilation audit once a year, especially for high-throughput industrial facilities. One customer in Atlanta skipped the annual audit for two years, and during their third audit, we found that their HEPA filters had developed small tears, which were allowing fine stainless steel dust to pass through. They had replaced the filters themselves, but they didn’t know that the installation was done incorrectly, leading to tears. The audit caught that before the dust caused health issues for their operators, and replacing the filters properly fixed it.
There are also machine-specific adjustments you can make to reduce the amount of contaminants released, which in turn makes ventilation more effective. For example, when loading your CBF machine, don’t overfill the barrels—overfilling causes parts and media to spill, creating more dust and debris. We recommend filling barrels to 70-80% of their capacity, which is the sweet spot for uniform finishing and less spillage. Also, make sure your finishing compound is mixed correctly and not over-concentrated. Too much chemical compound can create more VOC fumes, which can overload your filtration system. We work with chemical suppliers to provide compound mixing guidelines tailored to each CBF machine model we sell, and following those has helped customers reduce fume output by up to 30%. Finally, when you unload the machine, do it slowly and over the exhaust vent. If you dump the barrel all at once, you’ll release a cloud of dust and fumes that your ventilation system might not catch fast enough. Taking 2 to 3 minutes to unload over the vent lets the system pull all contaminants away before they spread.
I’ve talked to dozens of operators who think that ventilation is a hassle that adds cost to their operation. But the data proves otherwise. Proper ventilation reduces worker absenteeism by up to 25% (from fewer respiratory issues), extends the life of your CBF machine and its components (by preventing dust buildup in motors and bearings), and helps you avoid costly OSHA fines or environmental regulatory penalties. Last year, a customer in Ohio was cited $12,000 for failing to meet air quality limits in their finishing area, and they told us that fixing their ventilation system cost them $8,500—less than the fine, plus they improved their production quality in the process.
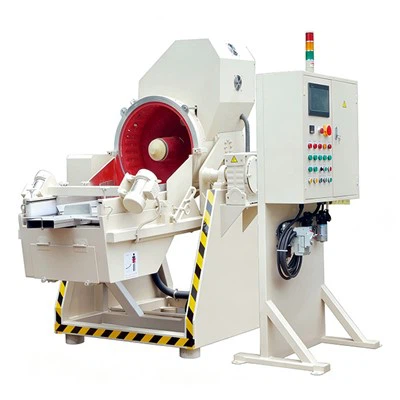
If you’re running a centrifugal barrel finishing machine and you’re concerned about ventilation, don’t wait until you have a compliance issue or an operator complaint. As a CBF machine supplier, we don’t just sell equipment—we provide ongoing support to help our customers run safe, efficient operations. To learn how to adapt ventilation to your specific CBF machine, part types, and production volume, reach out to our team to discuss your needs. We can help you design a ventilation system that fits your space and budget, provide training for your maintenance team, and support you with regular audits to keep your air quality compliant.
Grinding Polishing Machine Reference:
- Occupational Safety and Health Administration (OSHA). Ventilation in the Workplace: General Guidelines for Metal Finishing. OSHA 3467-07R-2019.
- centrifugal Barrel Finishing Association (CBFA). Best Practices for Workplace Air Quality in High-Volume Part Finishing. CBFA Technical Report 2022.
- National Institute for Occupational Safety and Health (NIOSH). Respirable Dust Control in Metal Tumbling Operations. NIOSH Publication No. 2021-105.
- American Conference of Governmental Industrial Hygienists (ACGIH). Threshold Limit Values for Chemical Substances and Physical Agents, 2023 Edition.
Dongguan Xindingsheng Intelligent Grinding Technology Co., Ltd.
Dongguan Xindingsheng Intelligent Grinding Technology Co., Ltd. is one of the most reliable centrifugal barrel finishing machine manufacturers and suppliers in China, also supports customized service. Please feel free to wholesale bulk high quality centrifugal barrel finishing machine in stock here from our factory. Contact us for pricelist.
Address: Room 101, Building 1, No. 73 Dahuangmei Road, Dalingshan Town, Dongguan City, Guangdong Province, China
E-mail: cndskj@126.com
WebSite: https://www.xdsfinishing.com/
